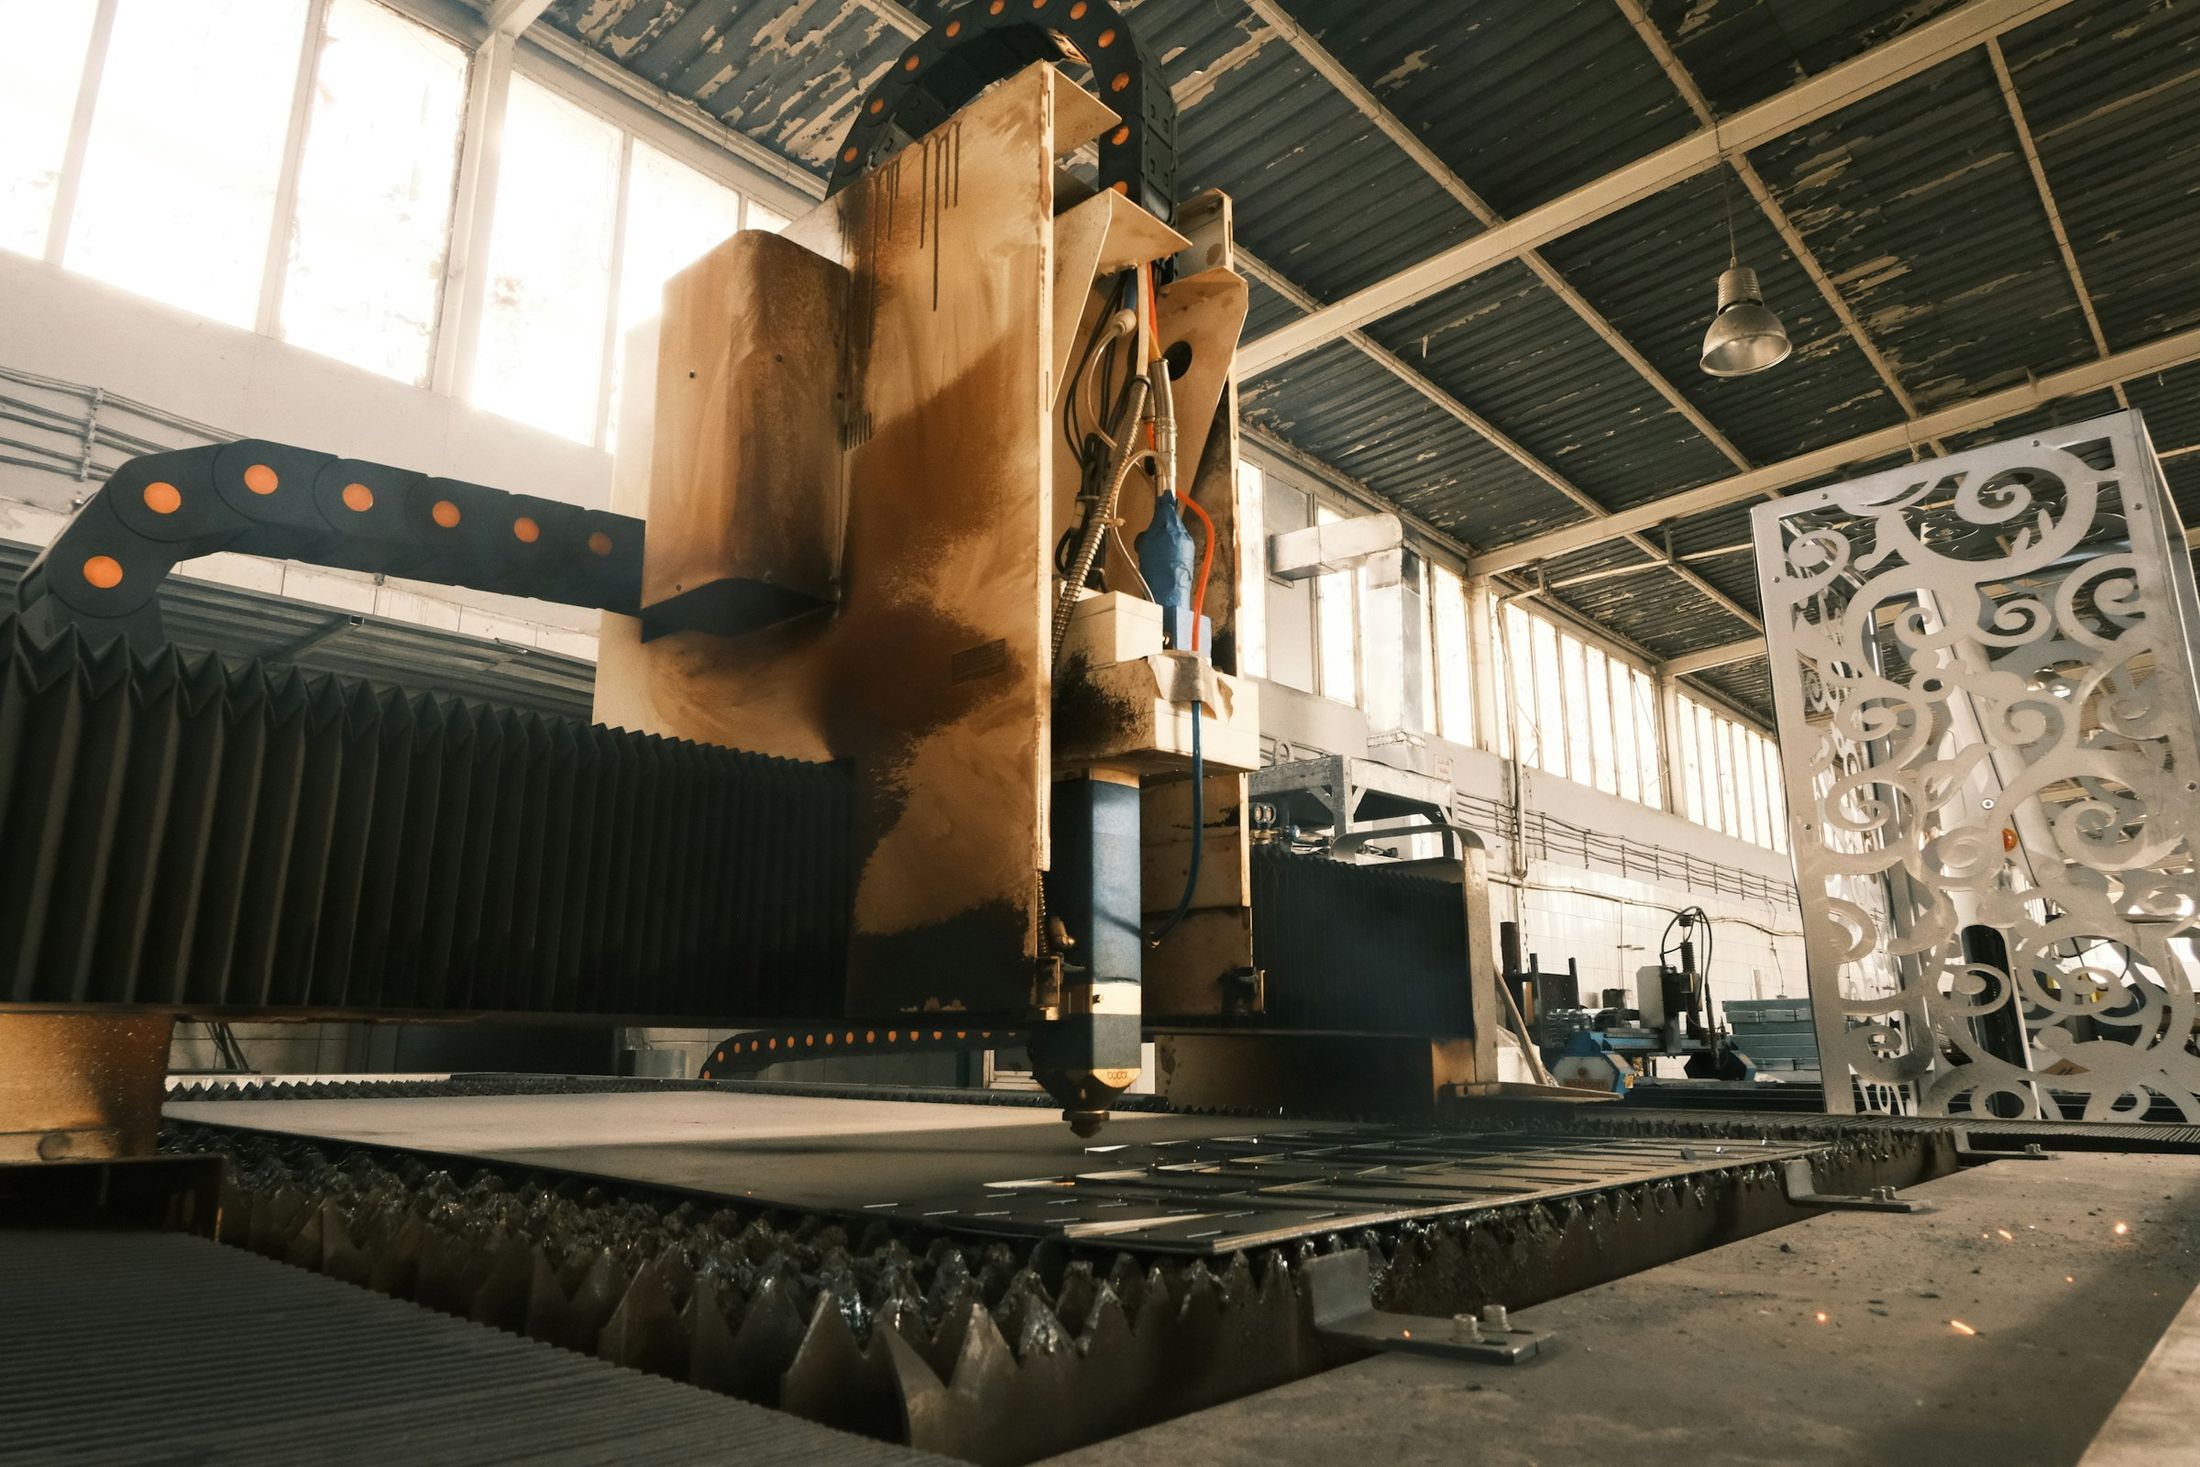
Laser cutting machine gantry over a slatted cutting bed in a bright shop bay

Seven operations · one building

Every op,in house.

Your part moves from the laser to the brake to the weld cell to the mill on carts, not trucks. One router, one traveler and one set of people who answer for it.

Largest blank5 x 12 ft
Max plate (plasma)1-1/4 in
Brake tonnage220 ton
Tightest held±0.0005 in
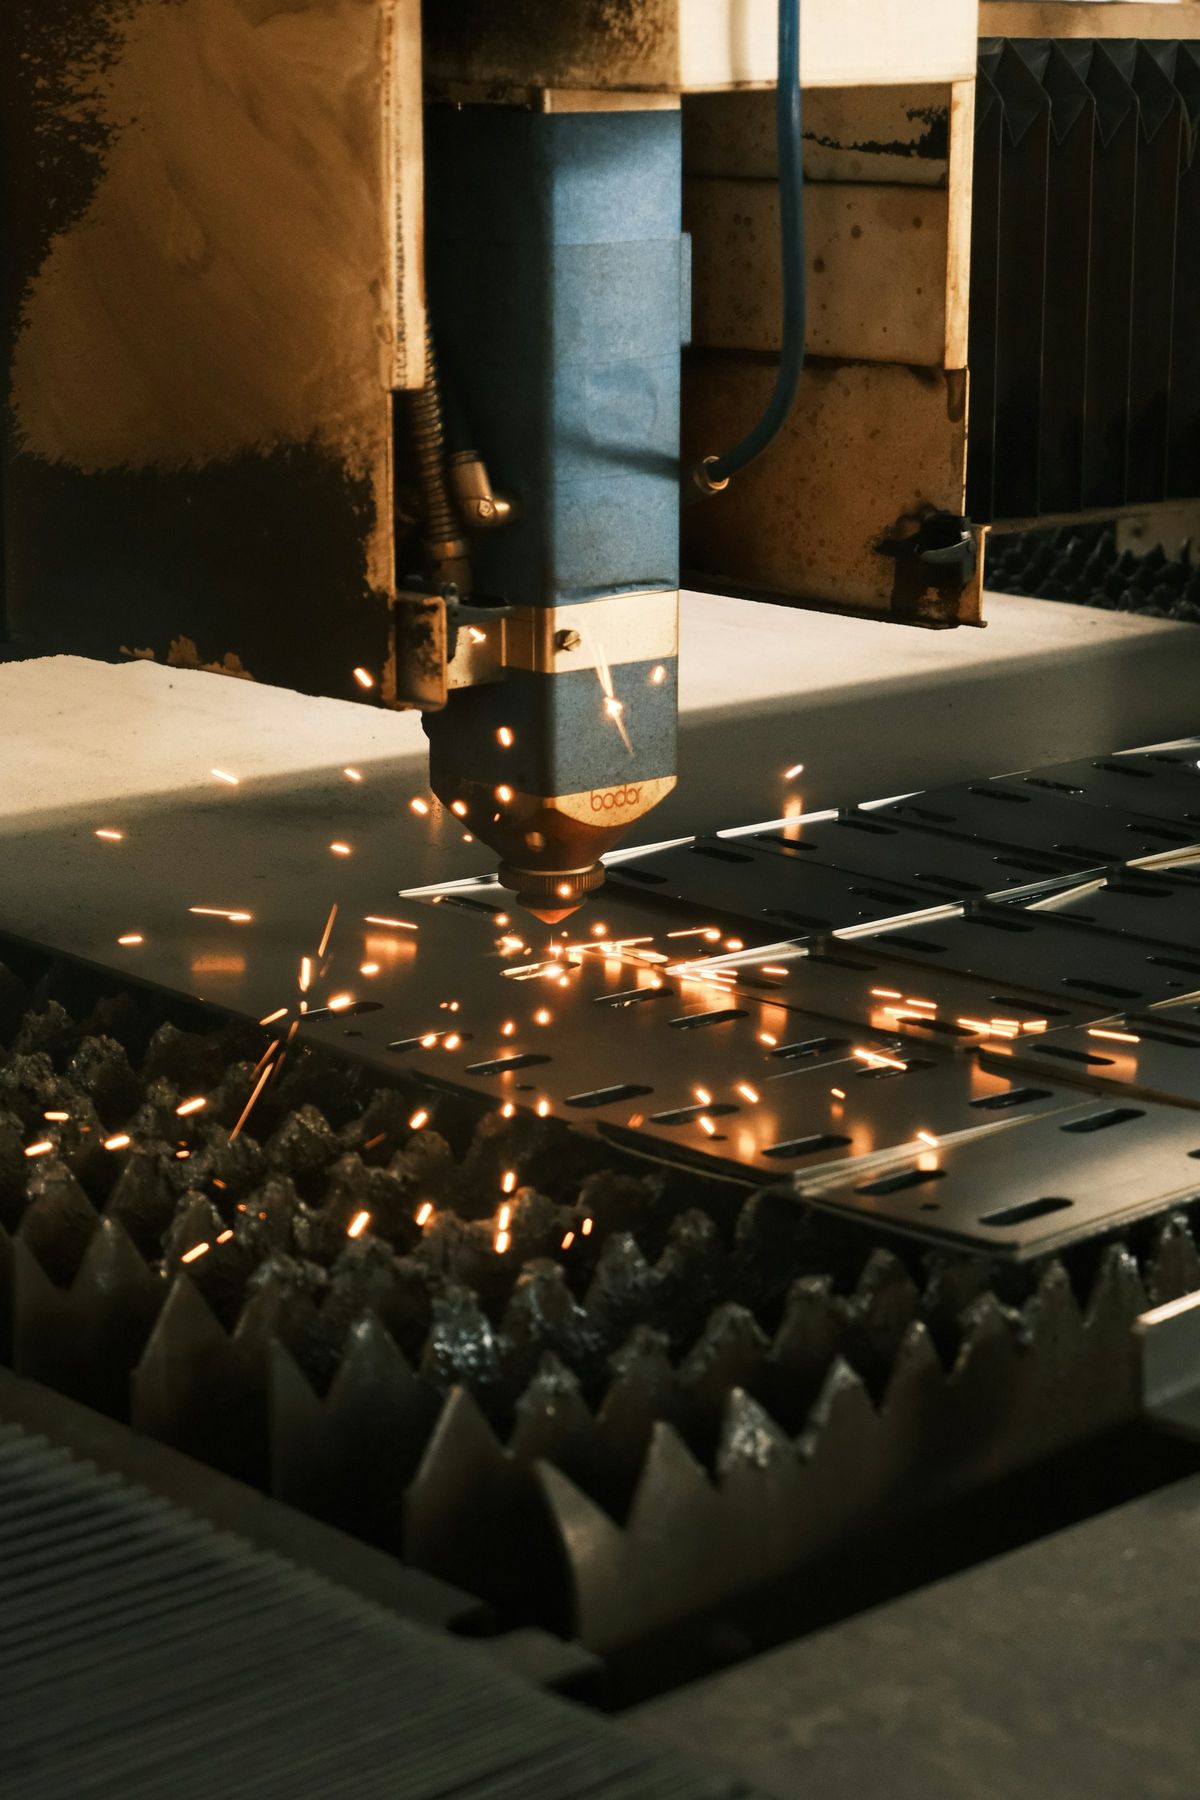
Laser cutting head throwing sparks over a slatted bed of cut steel

OP-10

Laser & plasma cutting

Two fiber lasers run sheet and light plate all day, nested by our programmers to get the most parts out of every sheet, with remnants tagged by heat number. Heavier plate goes to high-definition plasma with bevel capability.

Fiber laser
6 kW and 4 kW, 5 x 10 ft beds
Laser capacity
To 3/4 in mild steel, 5/8 in stainless, 1/2 in aluminum (6 kW)
Plasma
5 x 12 ft table, to 1-1/4 in, bevel head
Typical tolerance
±0.005 in laser on sheet, ±0.010 in on heavy plate, ±0.020 in plasma
Gloved hands positioning a steel sheet in a press brake

OP-20

Press brake forming

Four CNC brakes with back gauges and angle measurement. We keep a library of tooling for the radii our OEMs use most, so a repeat part sets up in minutes, not an hour.

Brakes
4 CNC, 90 to 220 ton, up to 12 ft
Angle tolerance
±0.5° standard, ±0.25° on request
Flange tolerance
±0.010 in
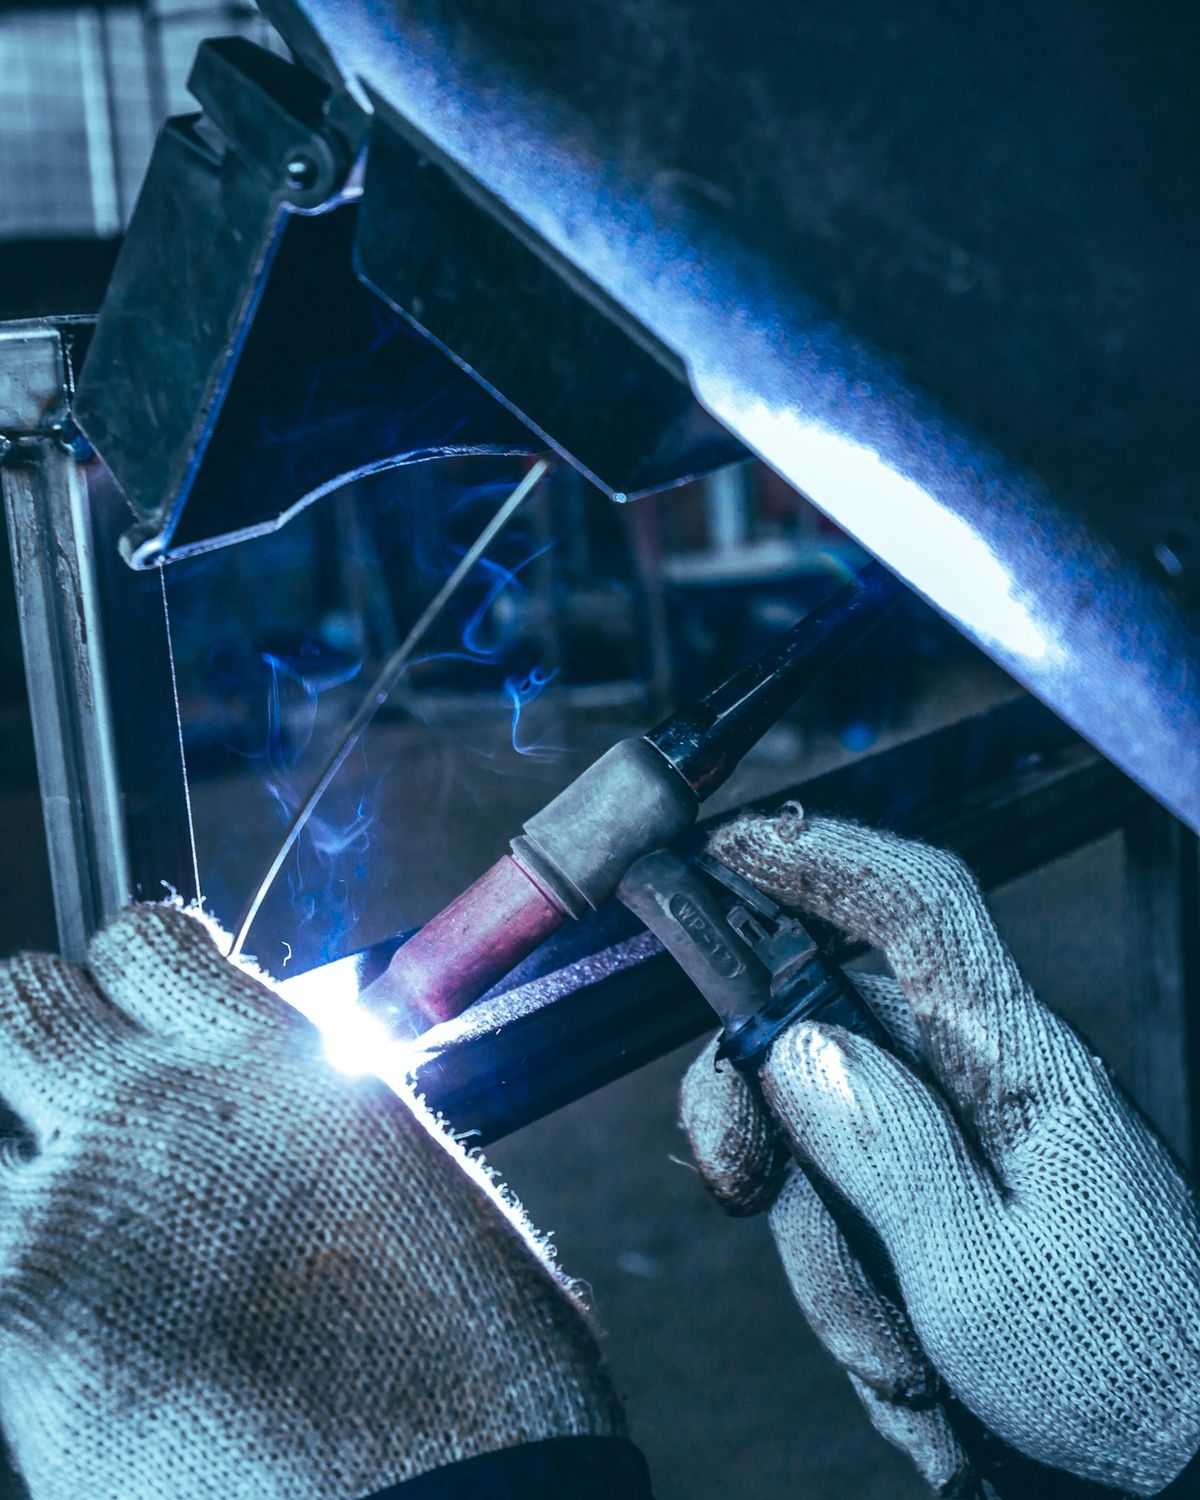
Close-up of gloved hands TIG welding a steel joint

OP-30

MIG & TIG welding

Fourteen manual cells and three robotic cells for the runs that repeat. Stainless food-contact work gets its own room, its own brushes and grinding discs, so carbon steel never touches it.

Processes
GMAW (MIG), GTAW (TIG), pulsed MIG
Materials
Carbon steel, 304 / 316 stainless, 5052 / 6061 aluminum
Certification
9 welders qualified to AWS D1.1 (steel), D1.2 (aluminum) and D1.6 (stainless)
Robotic cells
3, with dedicated fixtures per part number
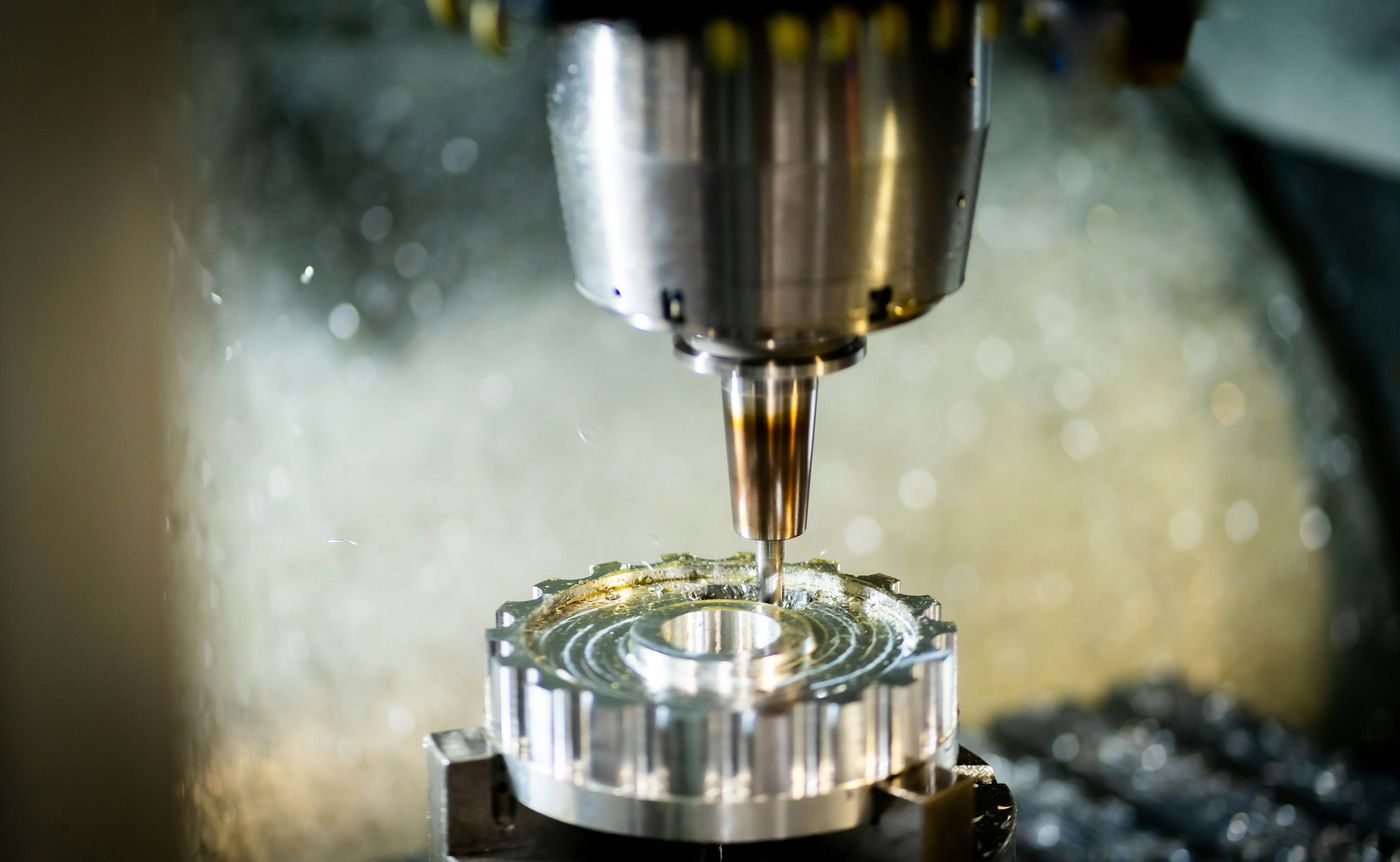
End mill cutting a round aluminum part in a CNC machining center

OP-40

CNC milling & turning

Machined features on weldments are why a lot of customers find us: the hub gets bored after welding, on the same floor, so distortion never becomes your problem.

Milling
6 vertical machining centers, two 5-axis
Turning
4 CNC lathes, two with live tooling, to 14 in turning diameter
Largest envelope
60 x 30 x 30 in
Tolerance
±0.005 in unless noted, ±0.001 in routine, ±0.0005 in on critical bores
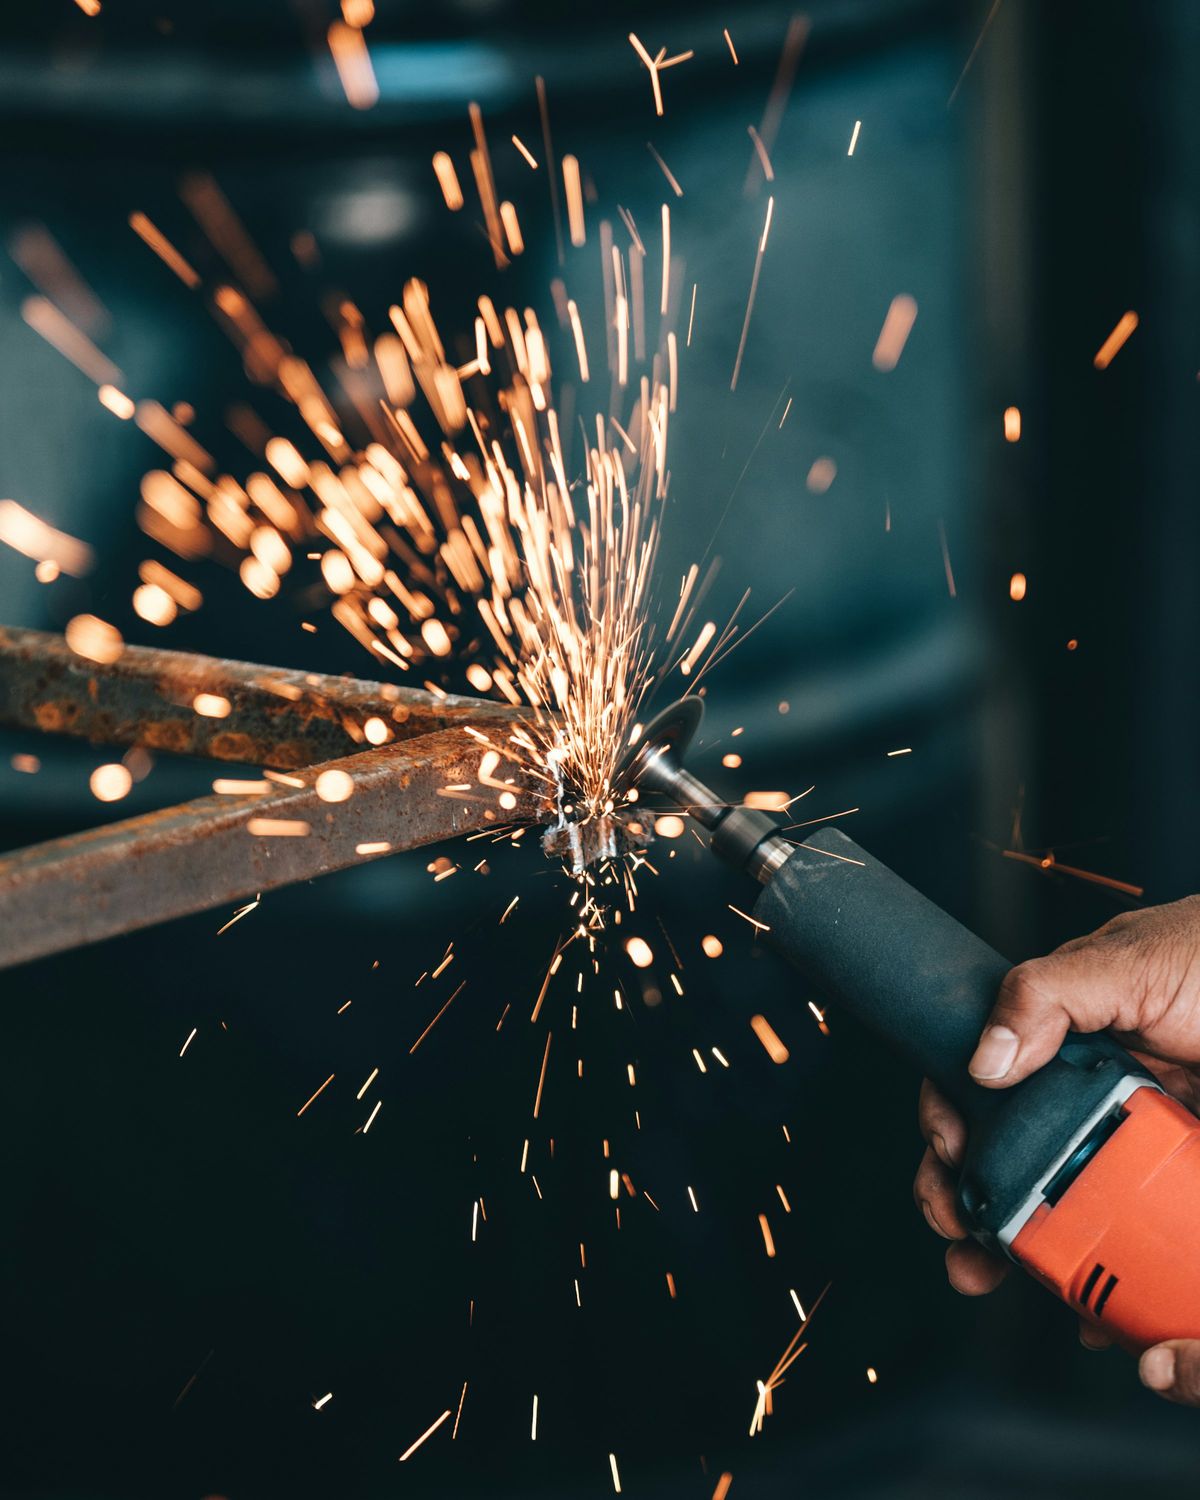
Angle grinder dressing a steel edge with sparks

OP-50

Finishing & powder coat

Deburring, graining and passivation happen here. Powder coat, plating and galvanizing go to three Lancaster County finishers we have used for over a decade, and we manage the schedule and the paperwork.

In house
Tumble deburr, wide-belt graining, #4 finish, passivation
Coordinated
Powder coat, zinc plate, hot-dip galvanize, anodize
Turnaround
Usually 3 to 7 working days added for outside finish
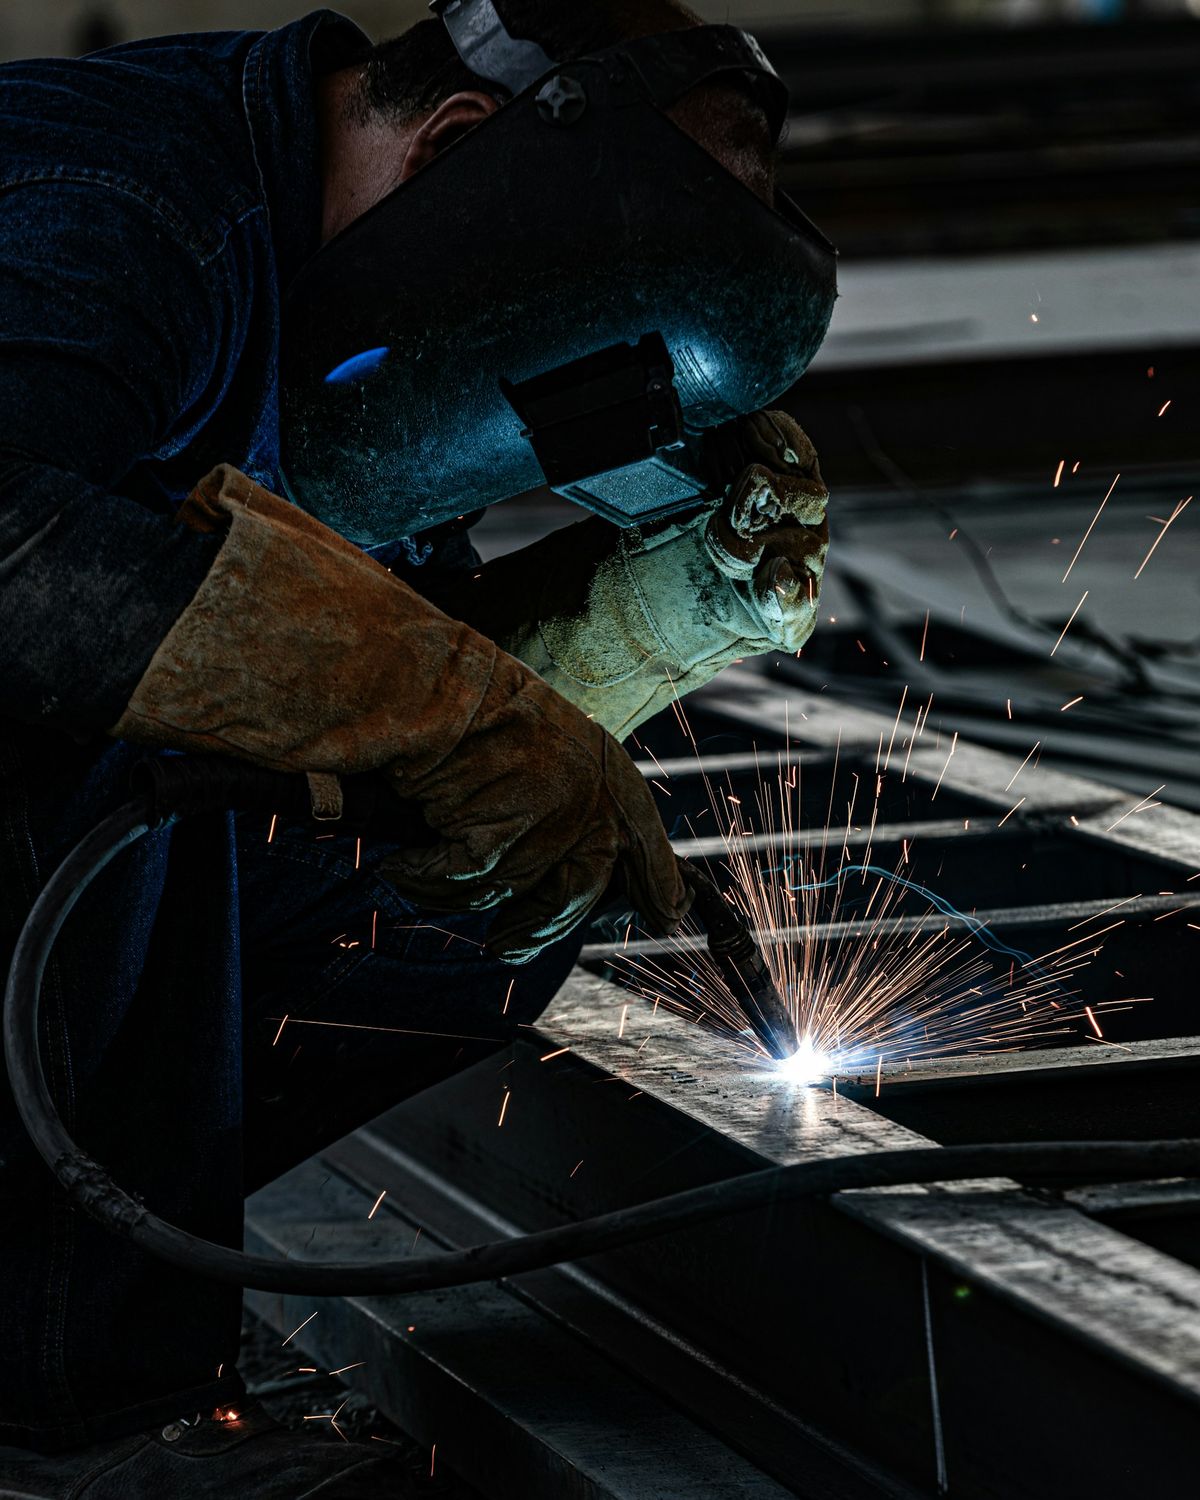
Welder tacking a steel frame on the assembly floor

OP-60

Assembly

Hardware, bearings, guards, sensors, wiring harnesses you supply: we put it together, check it against your BOM and ship it ready to bolt onto the machine.

Scope
Mechanical sub-assemblies, kitting, light electrical
Records
Serialized travelers, torque records on request
Packaging
Returnable racks, kanban bins, crating
Rows of machined steel flanges laid out on a table

All ops

Prototype to production

We like building the first one. Engineers get a part in hand in 5 to 10 days, we fix what the prototype teaches us, and the program, fixtures and inspection plan carry straight into the production run.

Prototypes
1 to 10 pieces, 5 to 10 business days
Production
25 to 5,000 per release, blanket orders welcome
Quality
FAI, CMM reports, PPAP on request

Materials by process

What we run, and where.

If your material is not on this chart, ask. If we can’t do it right, we will tell you who can.

MaterialOP-10
Cut
OP-20
Form
OP-30
Weld
OP-40
Machine
OP-50
Finish
Carbon steel (A36, 1018, 4140)YesYesYesYesCoordinated
Abrasion resistant (AR400, AR500)YesAR400 to 1/4 inYesDrill, tapCoordinated
Stainless (304, 316)YesYesYesYesPassivate
Aluminum (5052, 6061)Yes5052; 6061 limitedYesYesAnodize
Galvanneal, pre-galv sheetYesYesLimitedNoPaint, powder

In house With limits Coordinated with a finisher

Not sure which ops it needs?

Send the print. We’ll write the router.

Request a quote Or call the estimators (717) 958-3816